- Home /
- Food, Pharma & Cold Chain
UNILIFT-MHE In Food, Pharma & Cold Chain
Food, Pharma & Cold Chain
Retail & Supermarket Backroom: Efficient MHE for High-Traffic Environments
Unilift provides reliable lithium battery electric pallet trucks designed for supermarkets, retail backrooms, and distribution centers. With compact designs, quiet operation, and efficient performance, our equipment helps optimize goods movement from loading docks to shelves.
Key Applications
• Backroom Pallet Handling
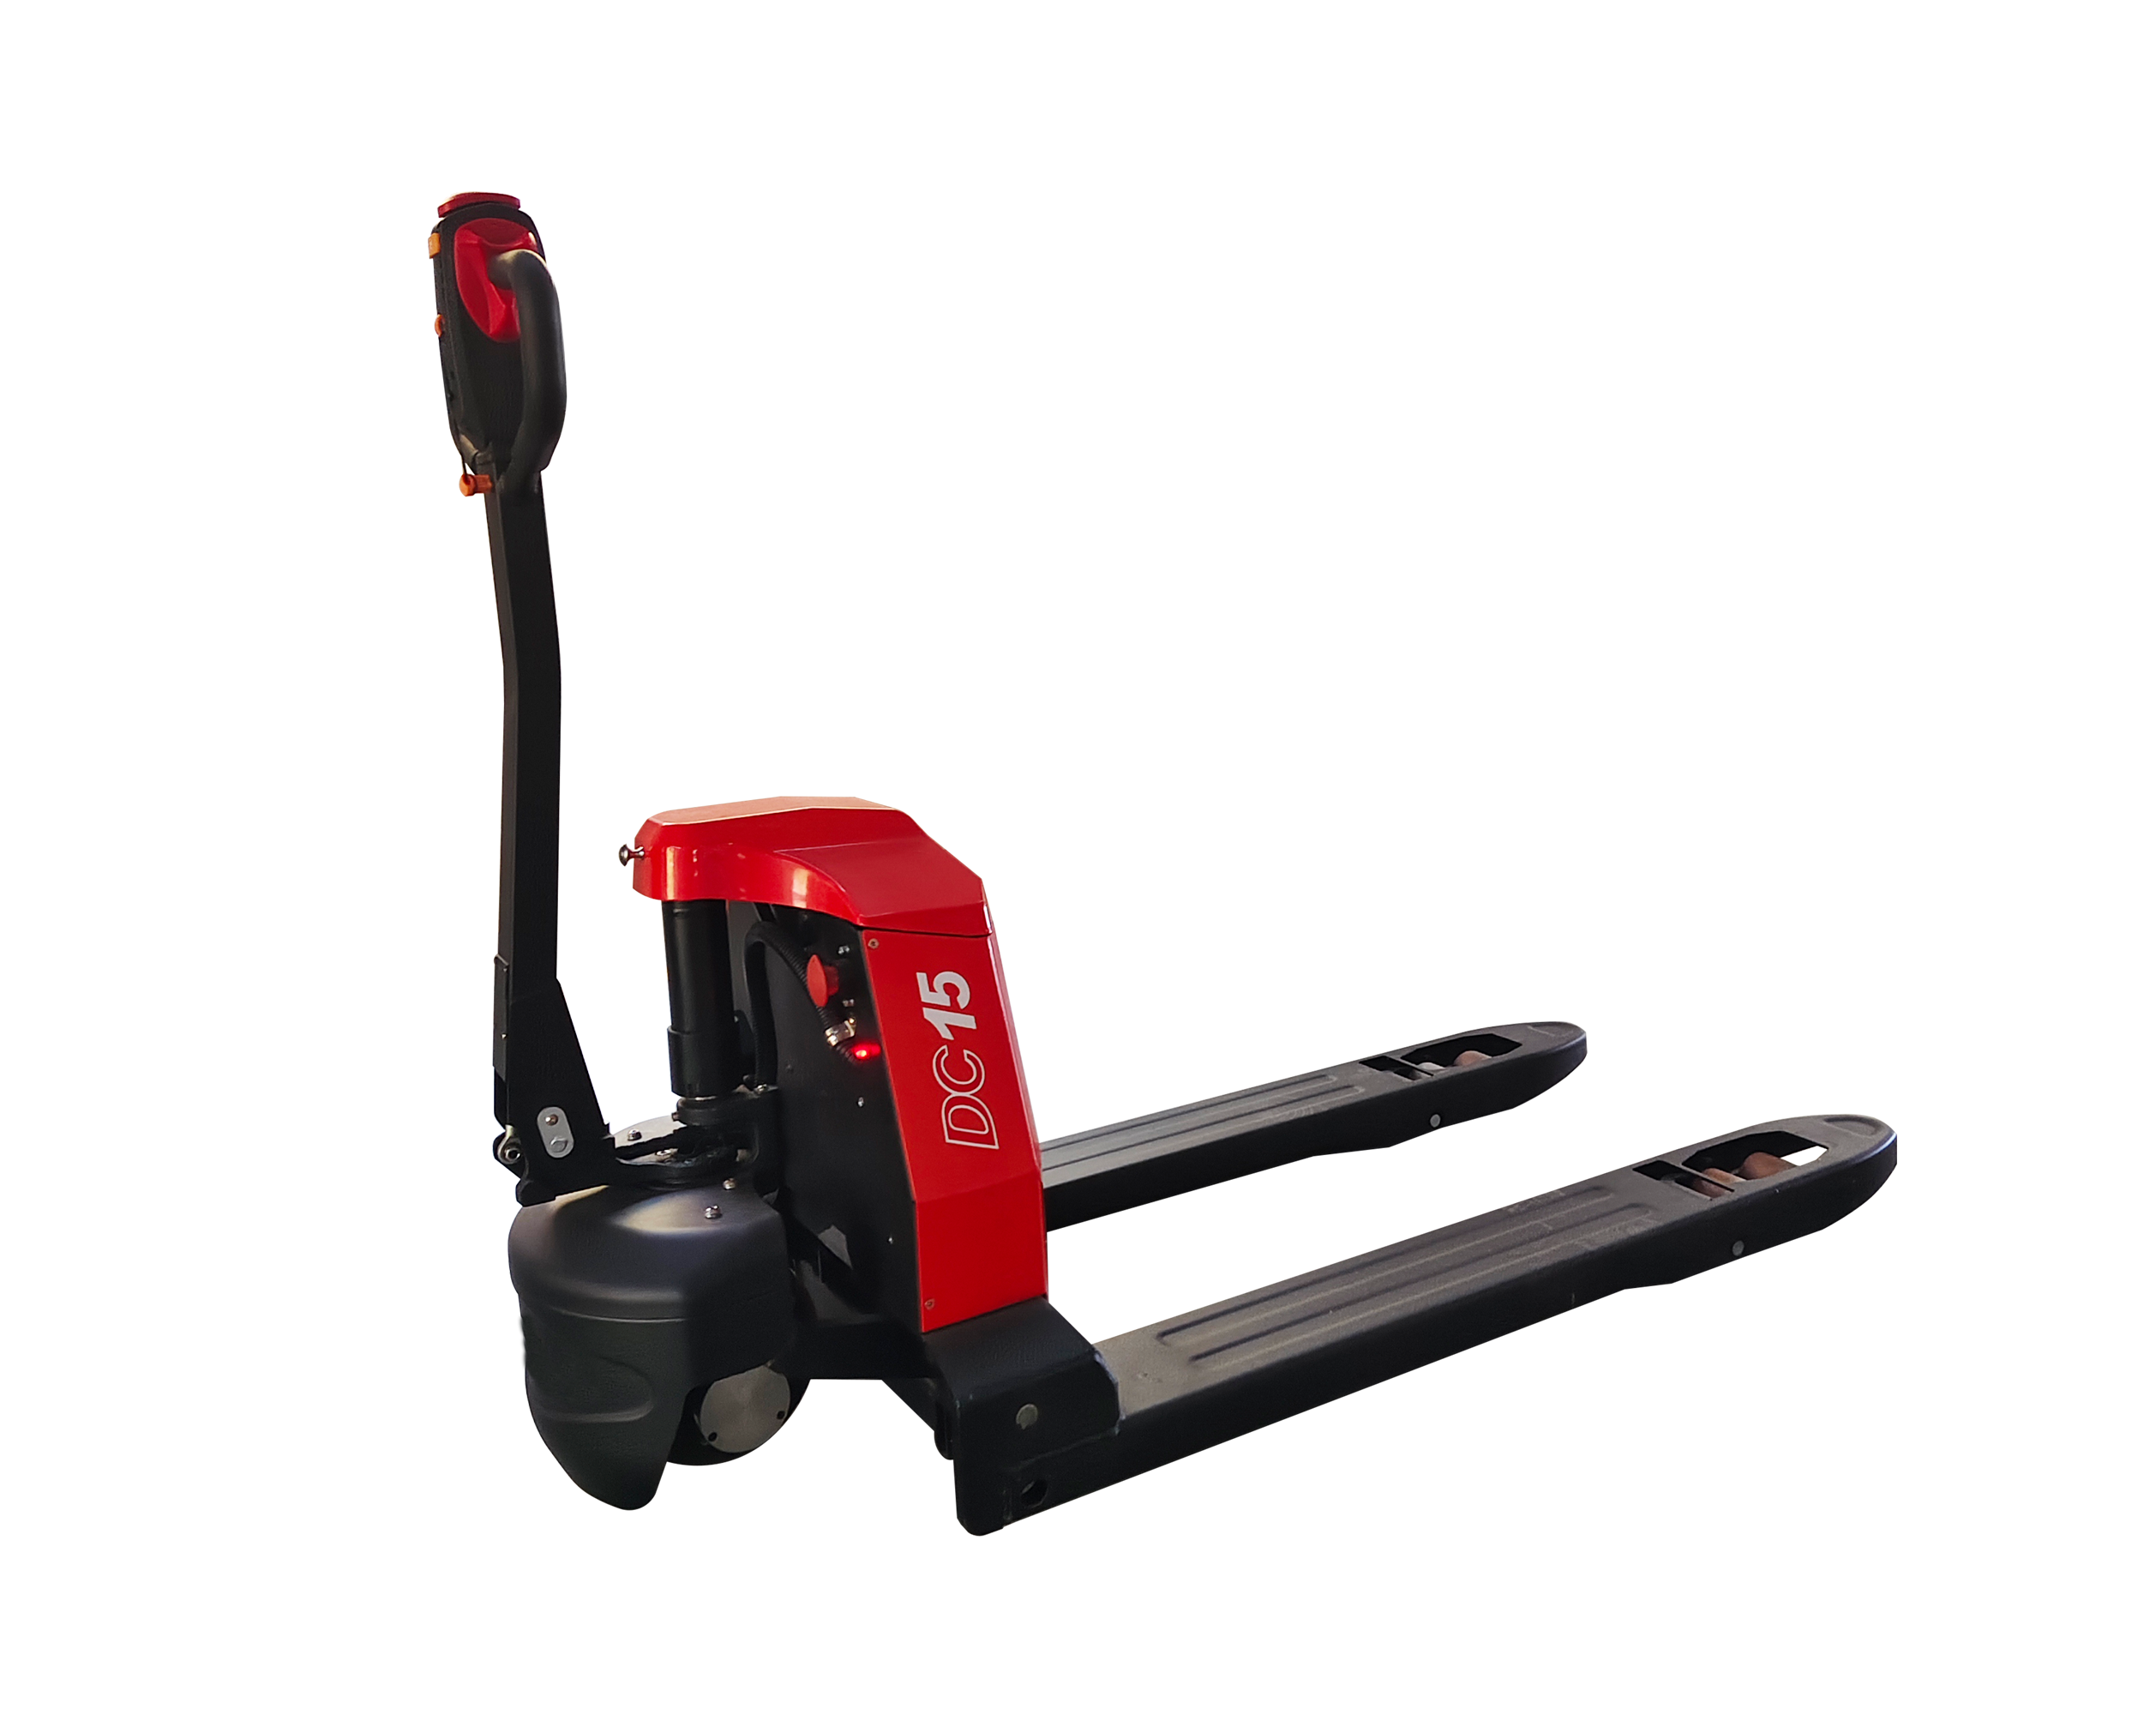
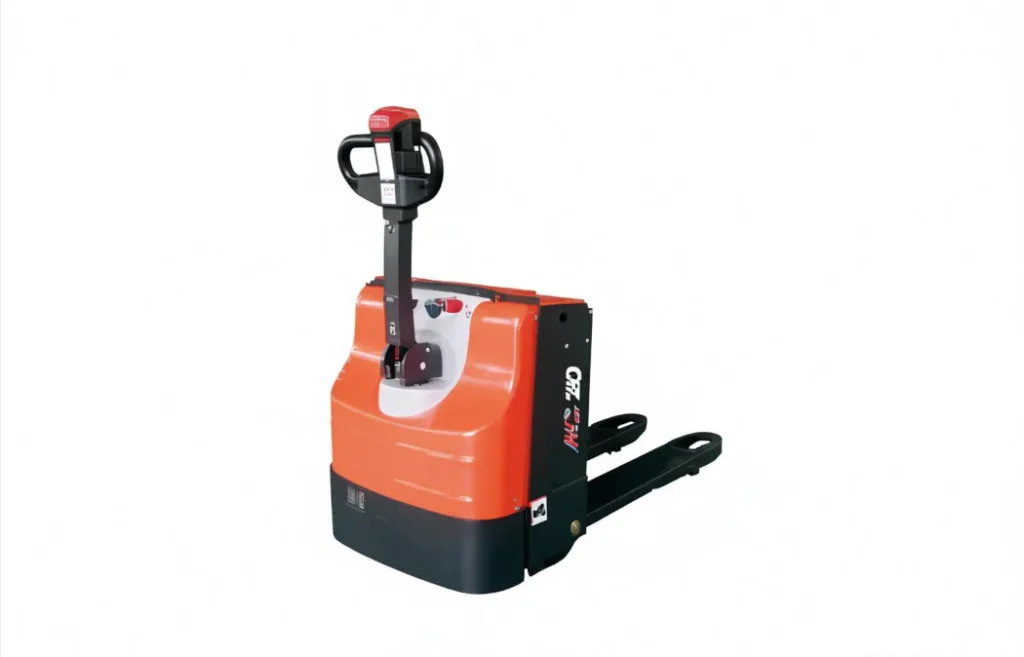
The CBD18/20-180(Li) Lithium Electric Pallet Truck (1.8–2 Ton) is ideal for daily pallet transport, shelf replenishment, and operations in limited spaces.
• High-Volume Retail Logistics
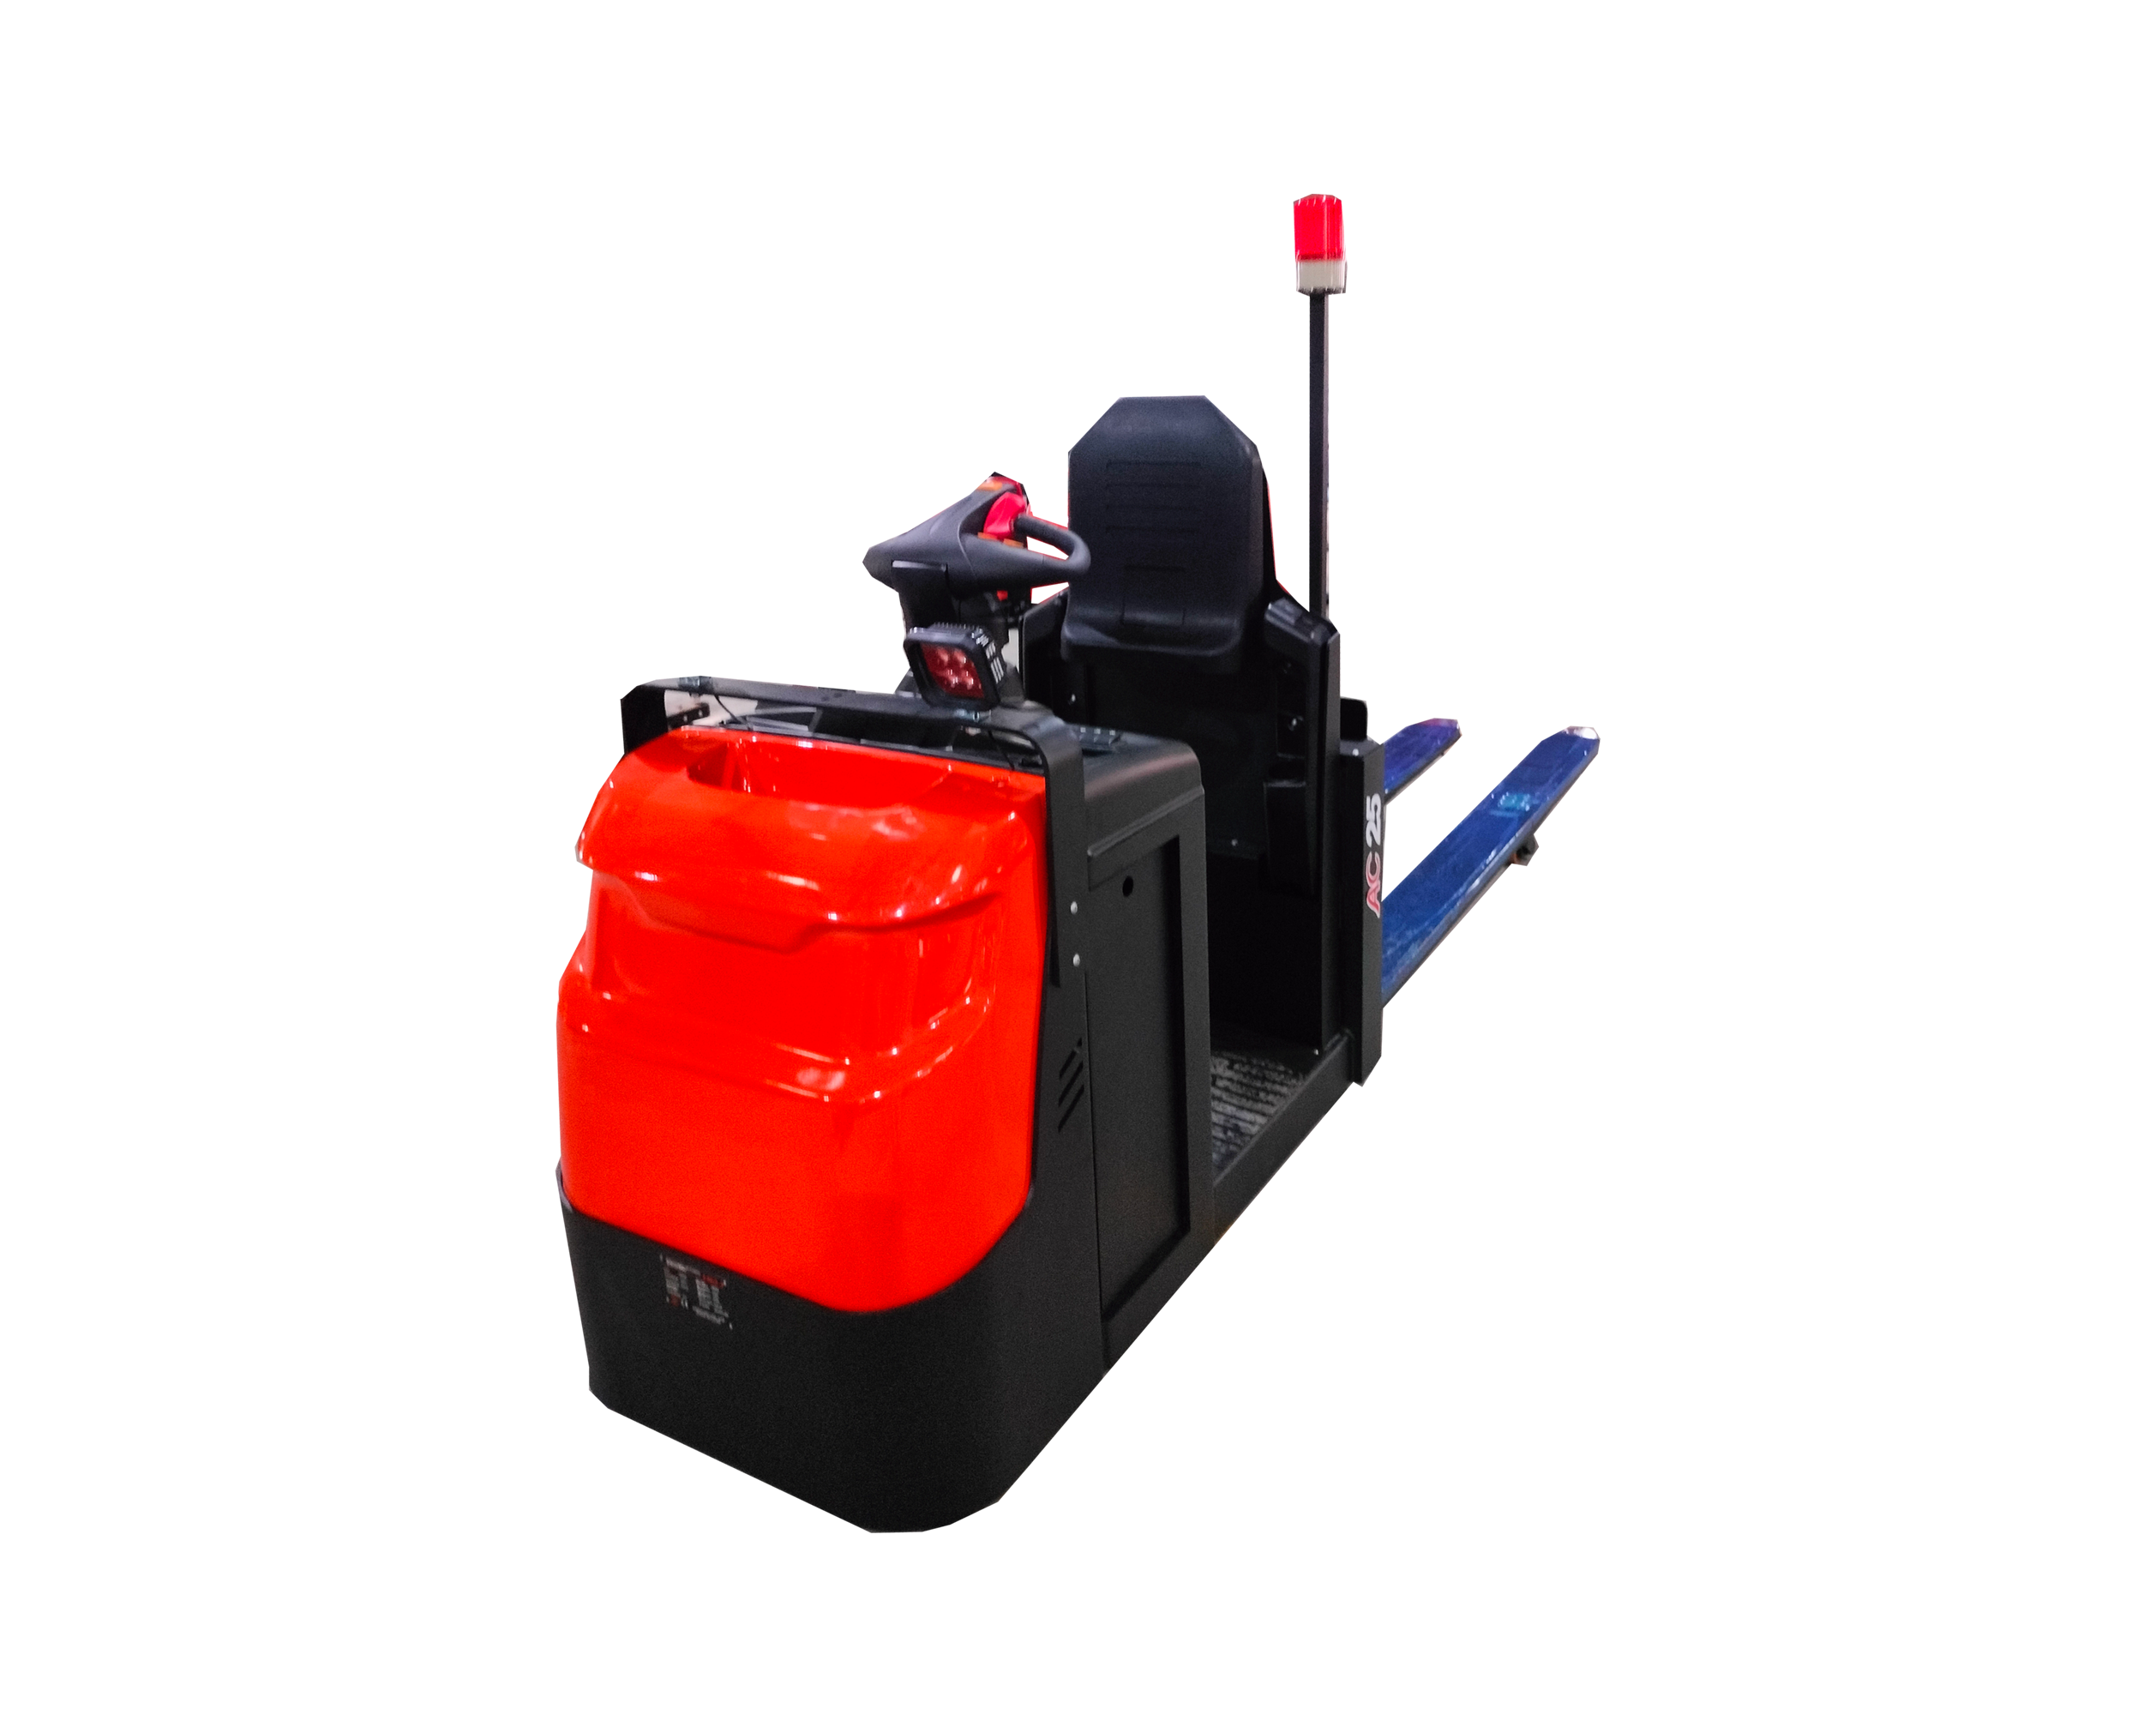
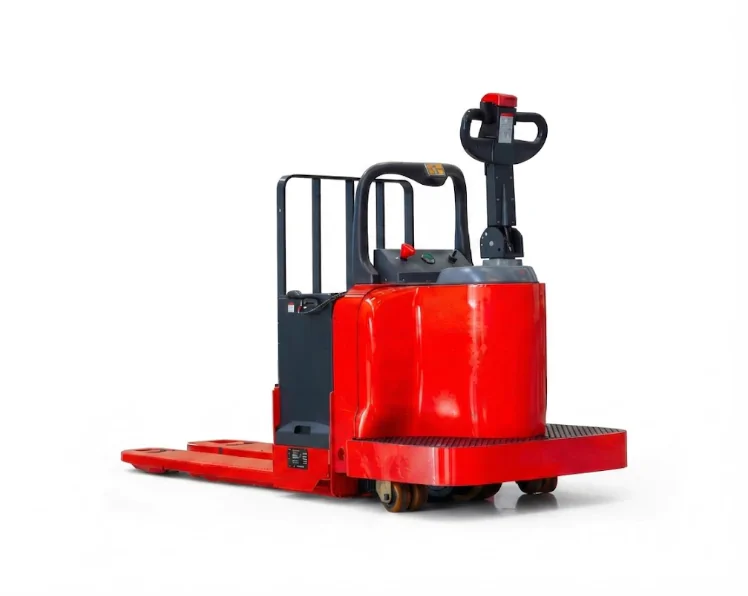
The CBD35-520(Li) 3.5 Ton Lithium Battery Stand-on Electric Pallet Truck delivers higher capacity and improved operator comfort for frequent pallet movement in large retail warehouses.
• Clean & Efficient Operation
Lithium battery technology provides low noise, zero emissions, fast charging, and reduced maintenance for modern retail environments.
Recommended Models:
- CBD18/20-180(Li): Compact retail and supermarket backroom handling
- CBD35-520(Li): Heavy-duty pallet transportation for large retail facilities
Food, Pharma & Cold Chain: Reliable MHE for Temperature-Controlled Environments
Food, Pharma & Cold Chain
Keeping Temperature-Sensitive Goods Moving Safely and Efficiently
In food, pharmaceutical, and cold chain logistics, material handling equipment must perform reliably in demanding environments where hygiene, temperature control, and operational efficiency are critical. Unilift MHE provides a range of electric material handling solutions designed to support the movement, storage, and order preparation of temperature-sensitive goods across warehouses, cold storage facilities, distribution centers, and production areas.
1. Optimized for Cold Chain Challenges
Our electric material handling equipment is designed to address the demanding conditions found in food, pharmaceutical, and temperature-controlled logistics:
Reliable Performance in Cold Environments: Electric pallet trucks and stackers can support daily material movement in temperature-controlled warehouses and cold storage areas.
Clean & Low-Emission Operation: Electric drive systems produce zero exhaust emissions during operation, making them suitable for enclosed warehouses and facilities where clean working environments are essential.
Compact Maneuverability: Compact equipment designs help operators move pallets efficiently through narrow aisles, storage areas, loading zones, and temperature-controlled rooms.
Ergonomic Operation: Intuitive controls and practical operator designs help reduce physical strain during repetitive pallet handling and order preparation.
Efficient Battery Solutions: Lithium battery configurations support frequent handling operations and can help reduce charging downtime when opportunity charging is available.
2. Key Application Scenarios
Unilift MHE supports multiple stages of the food, pharmaceutical, and cold chain logistics process:
Cold Storage Loading & Unloading
Move pallets efficiently between delivery vehicles, loading docks, staging areas, and temperature-controlled storage. Our Electric Pallet Trucks provide flexible handling for frequent pallet movement in confined areas.
Temperature-Controlled Warehouse Storage
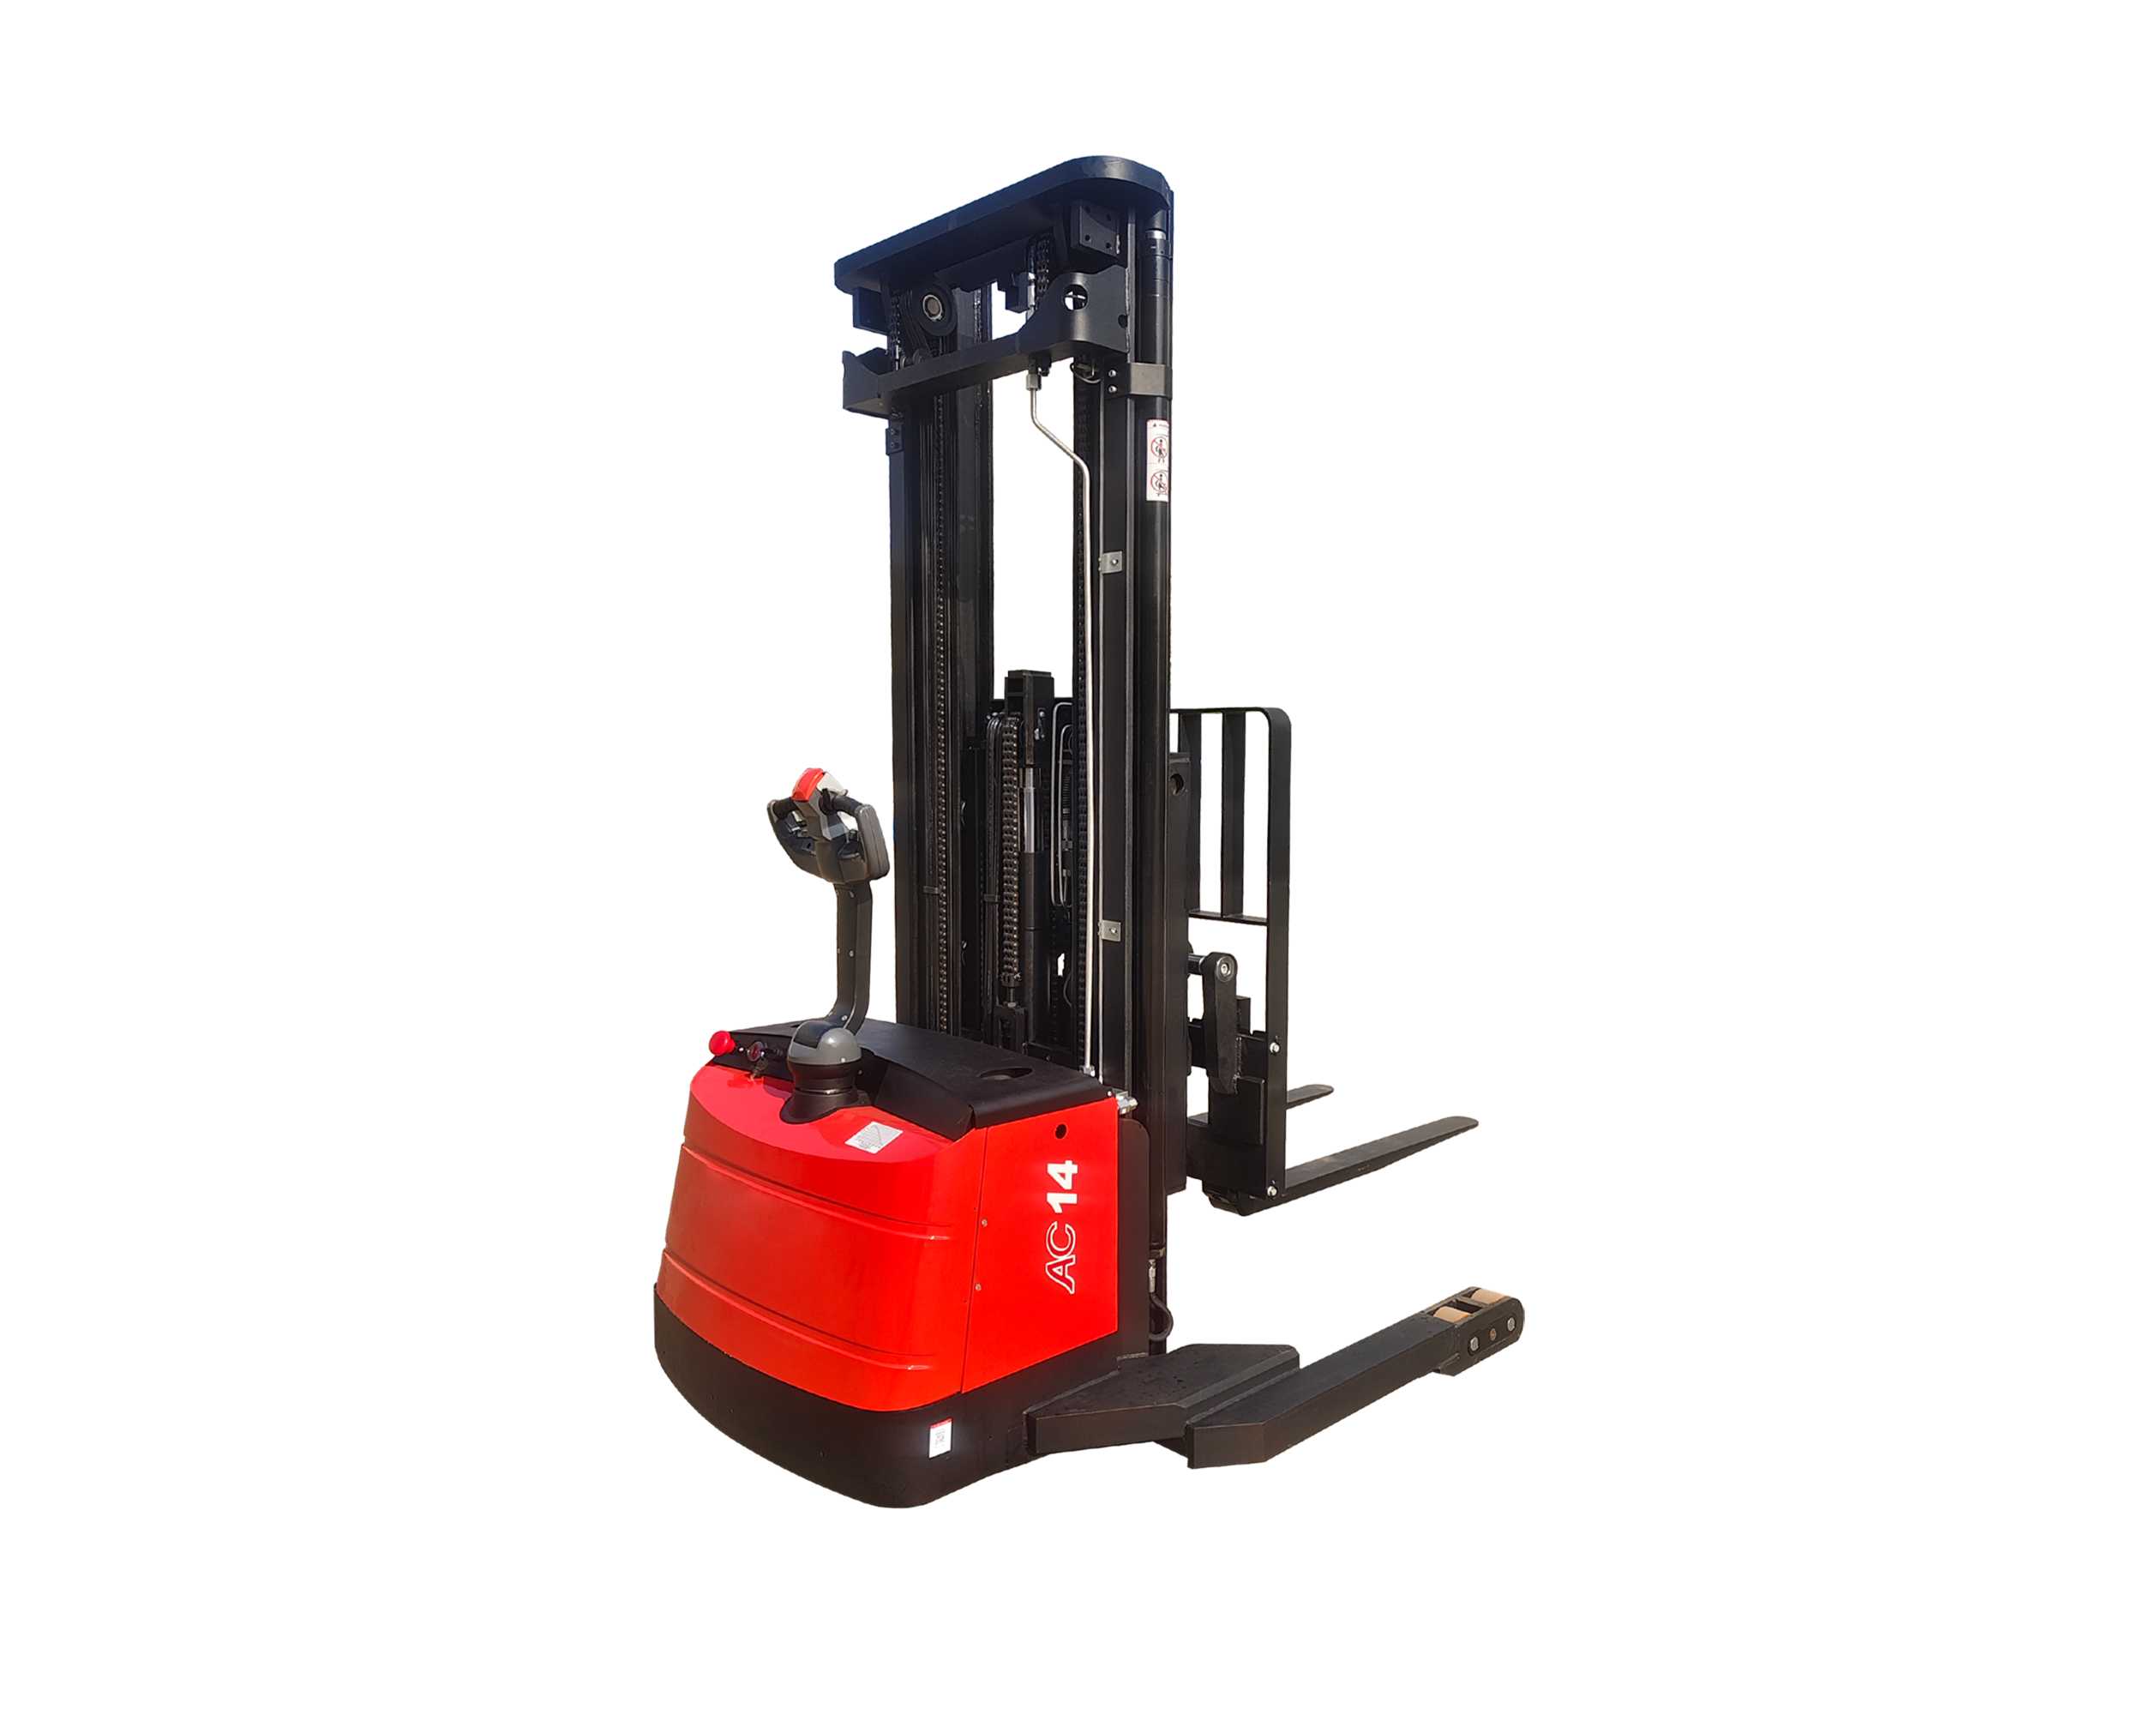
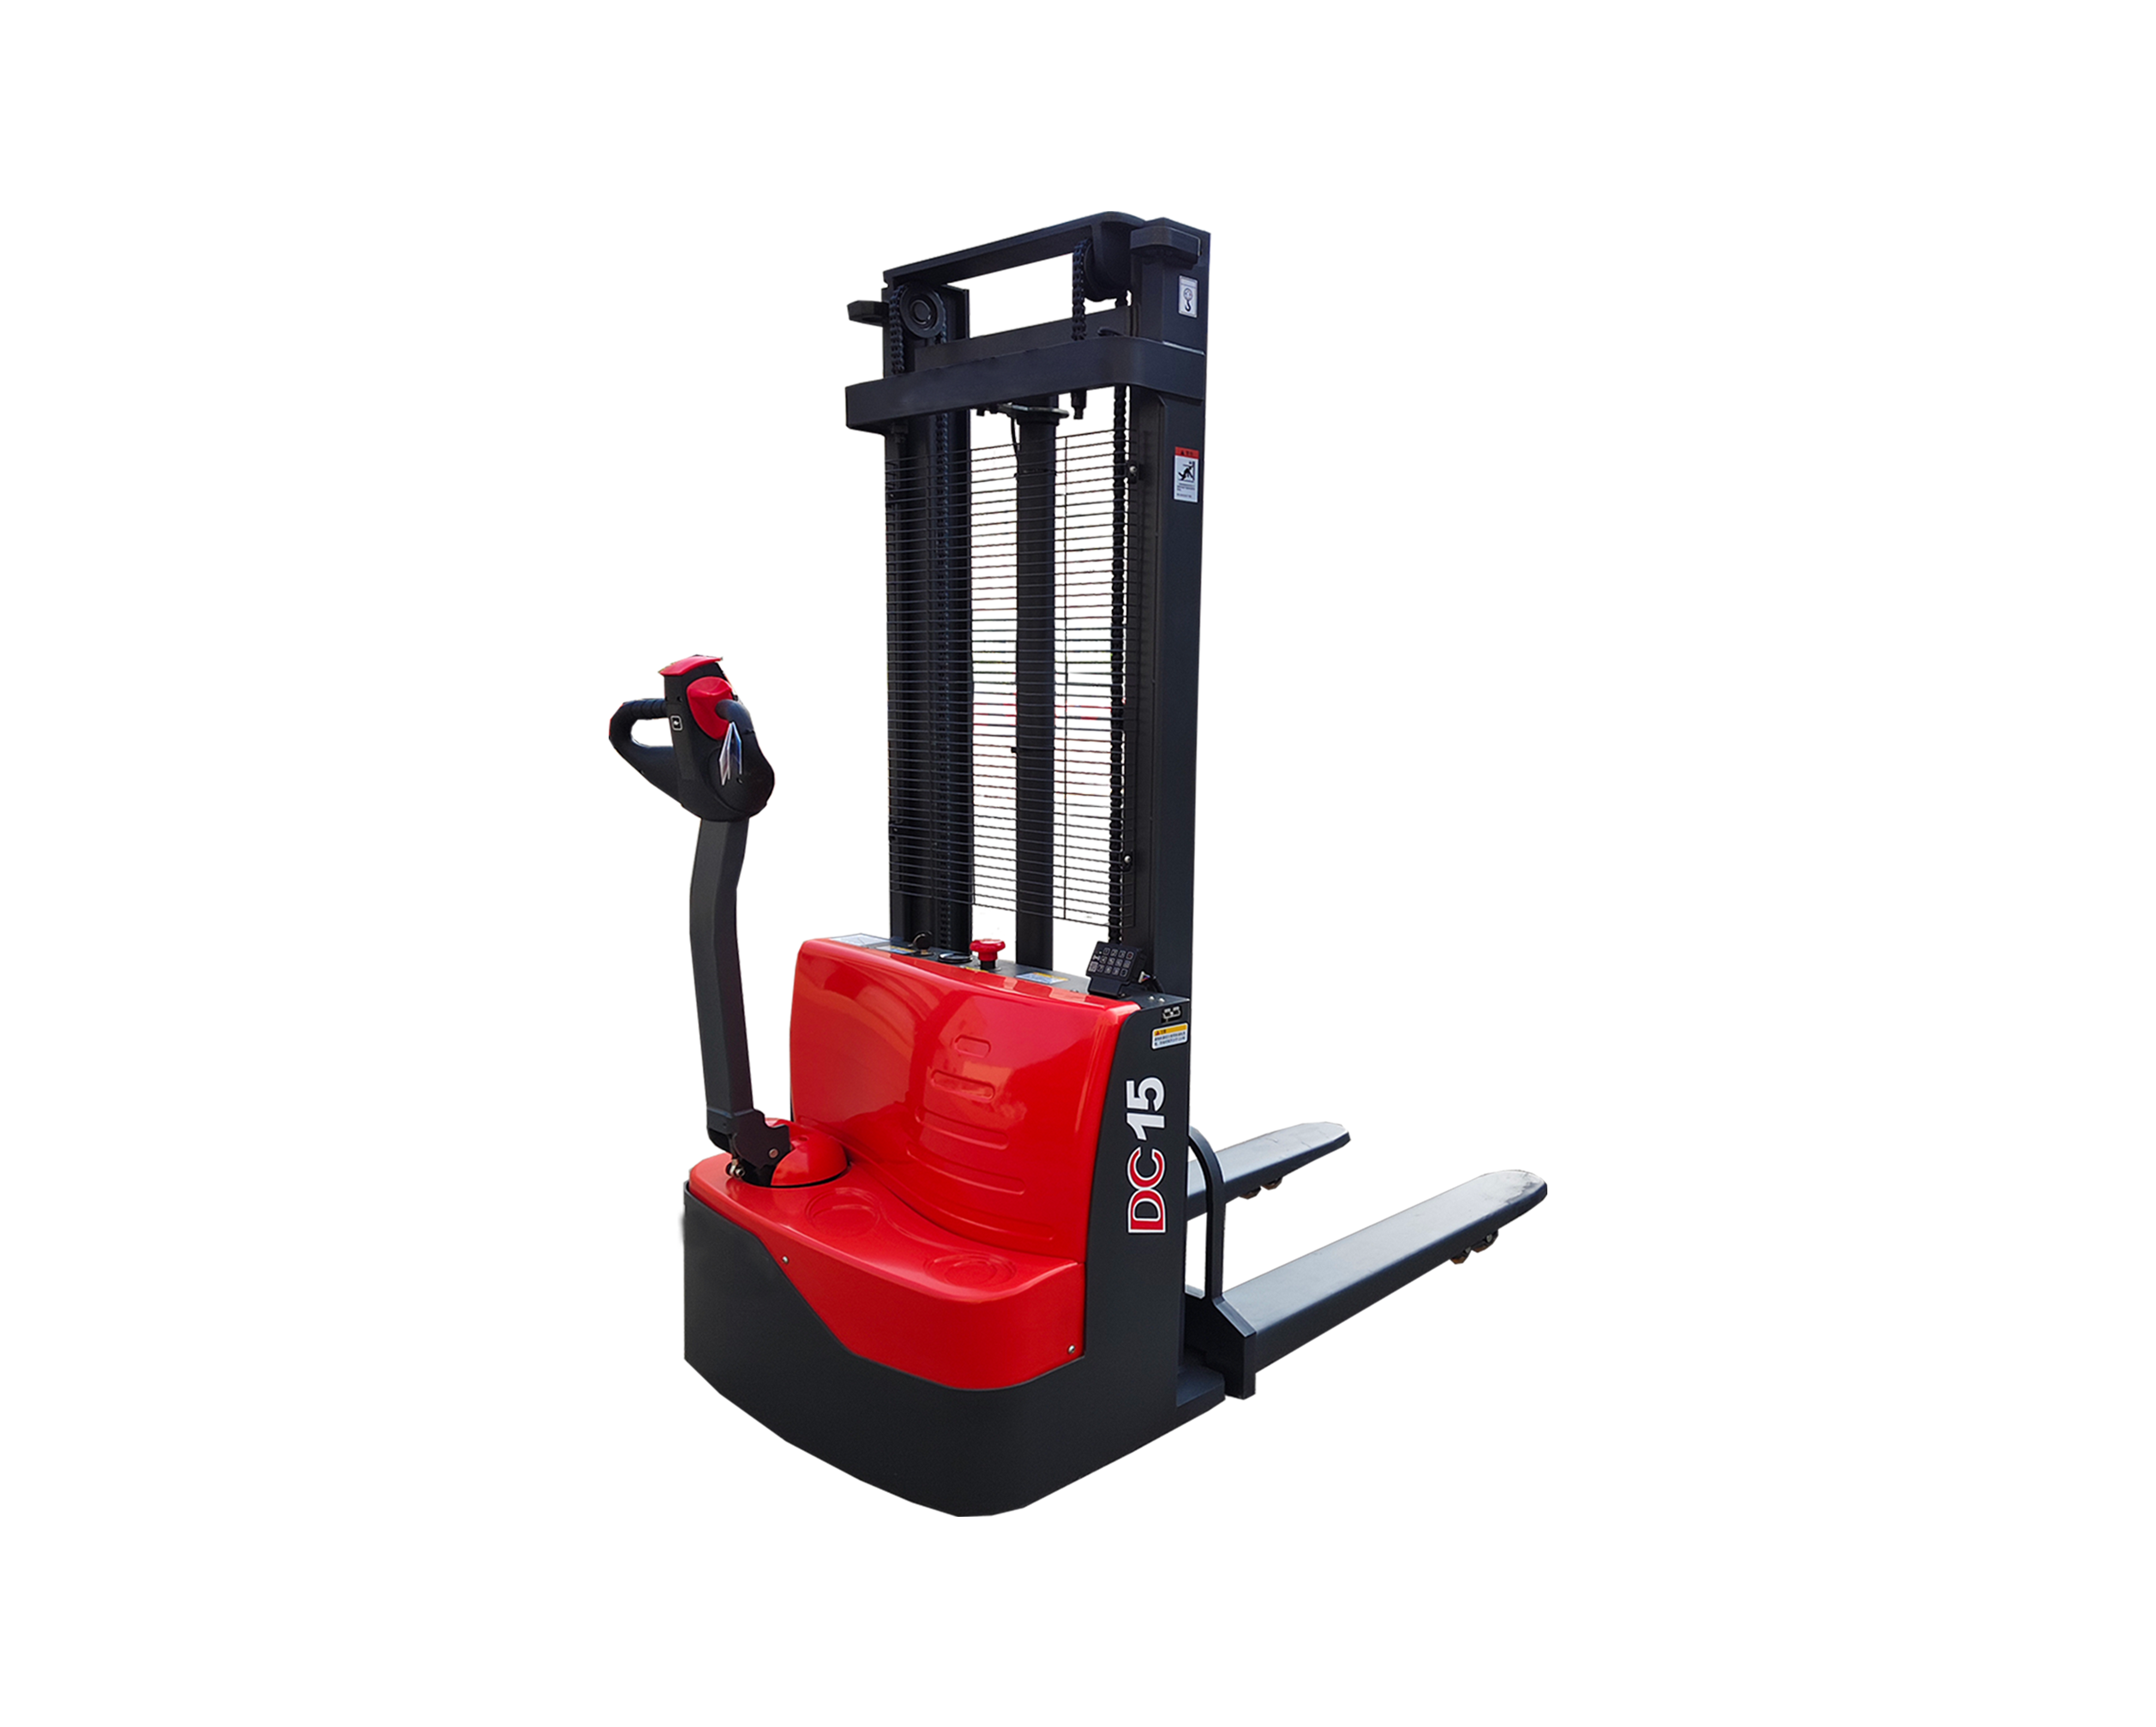
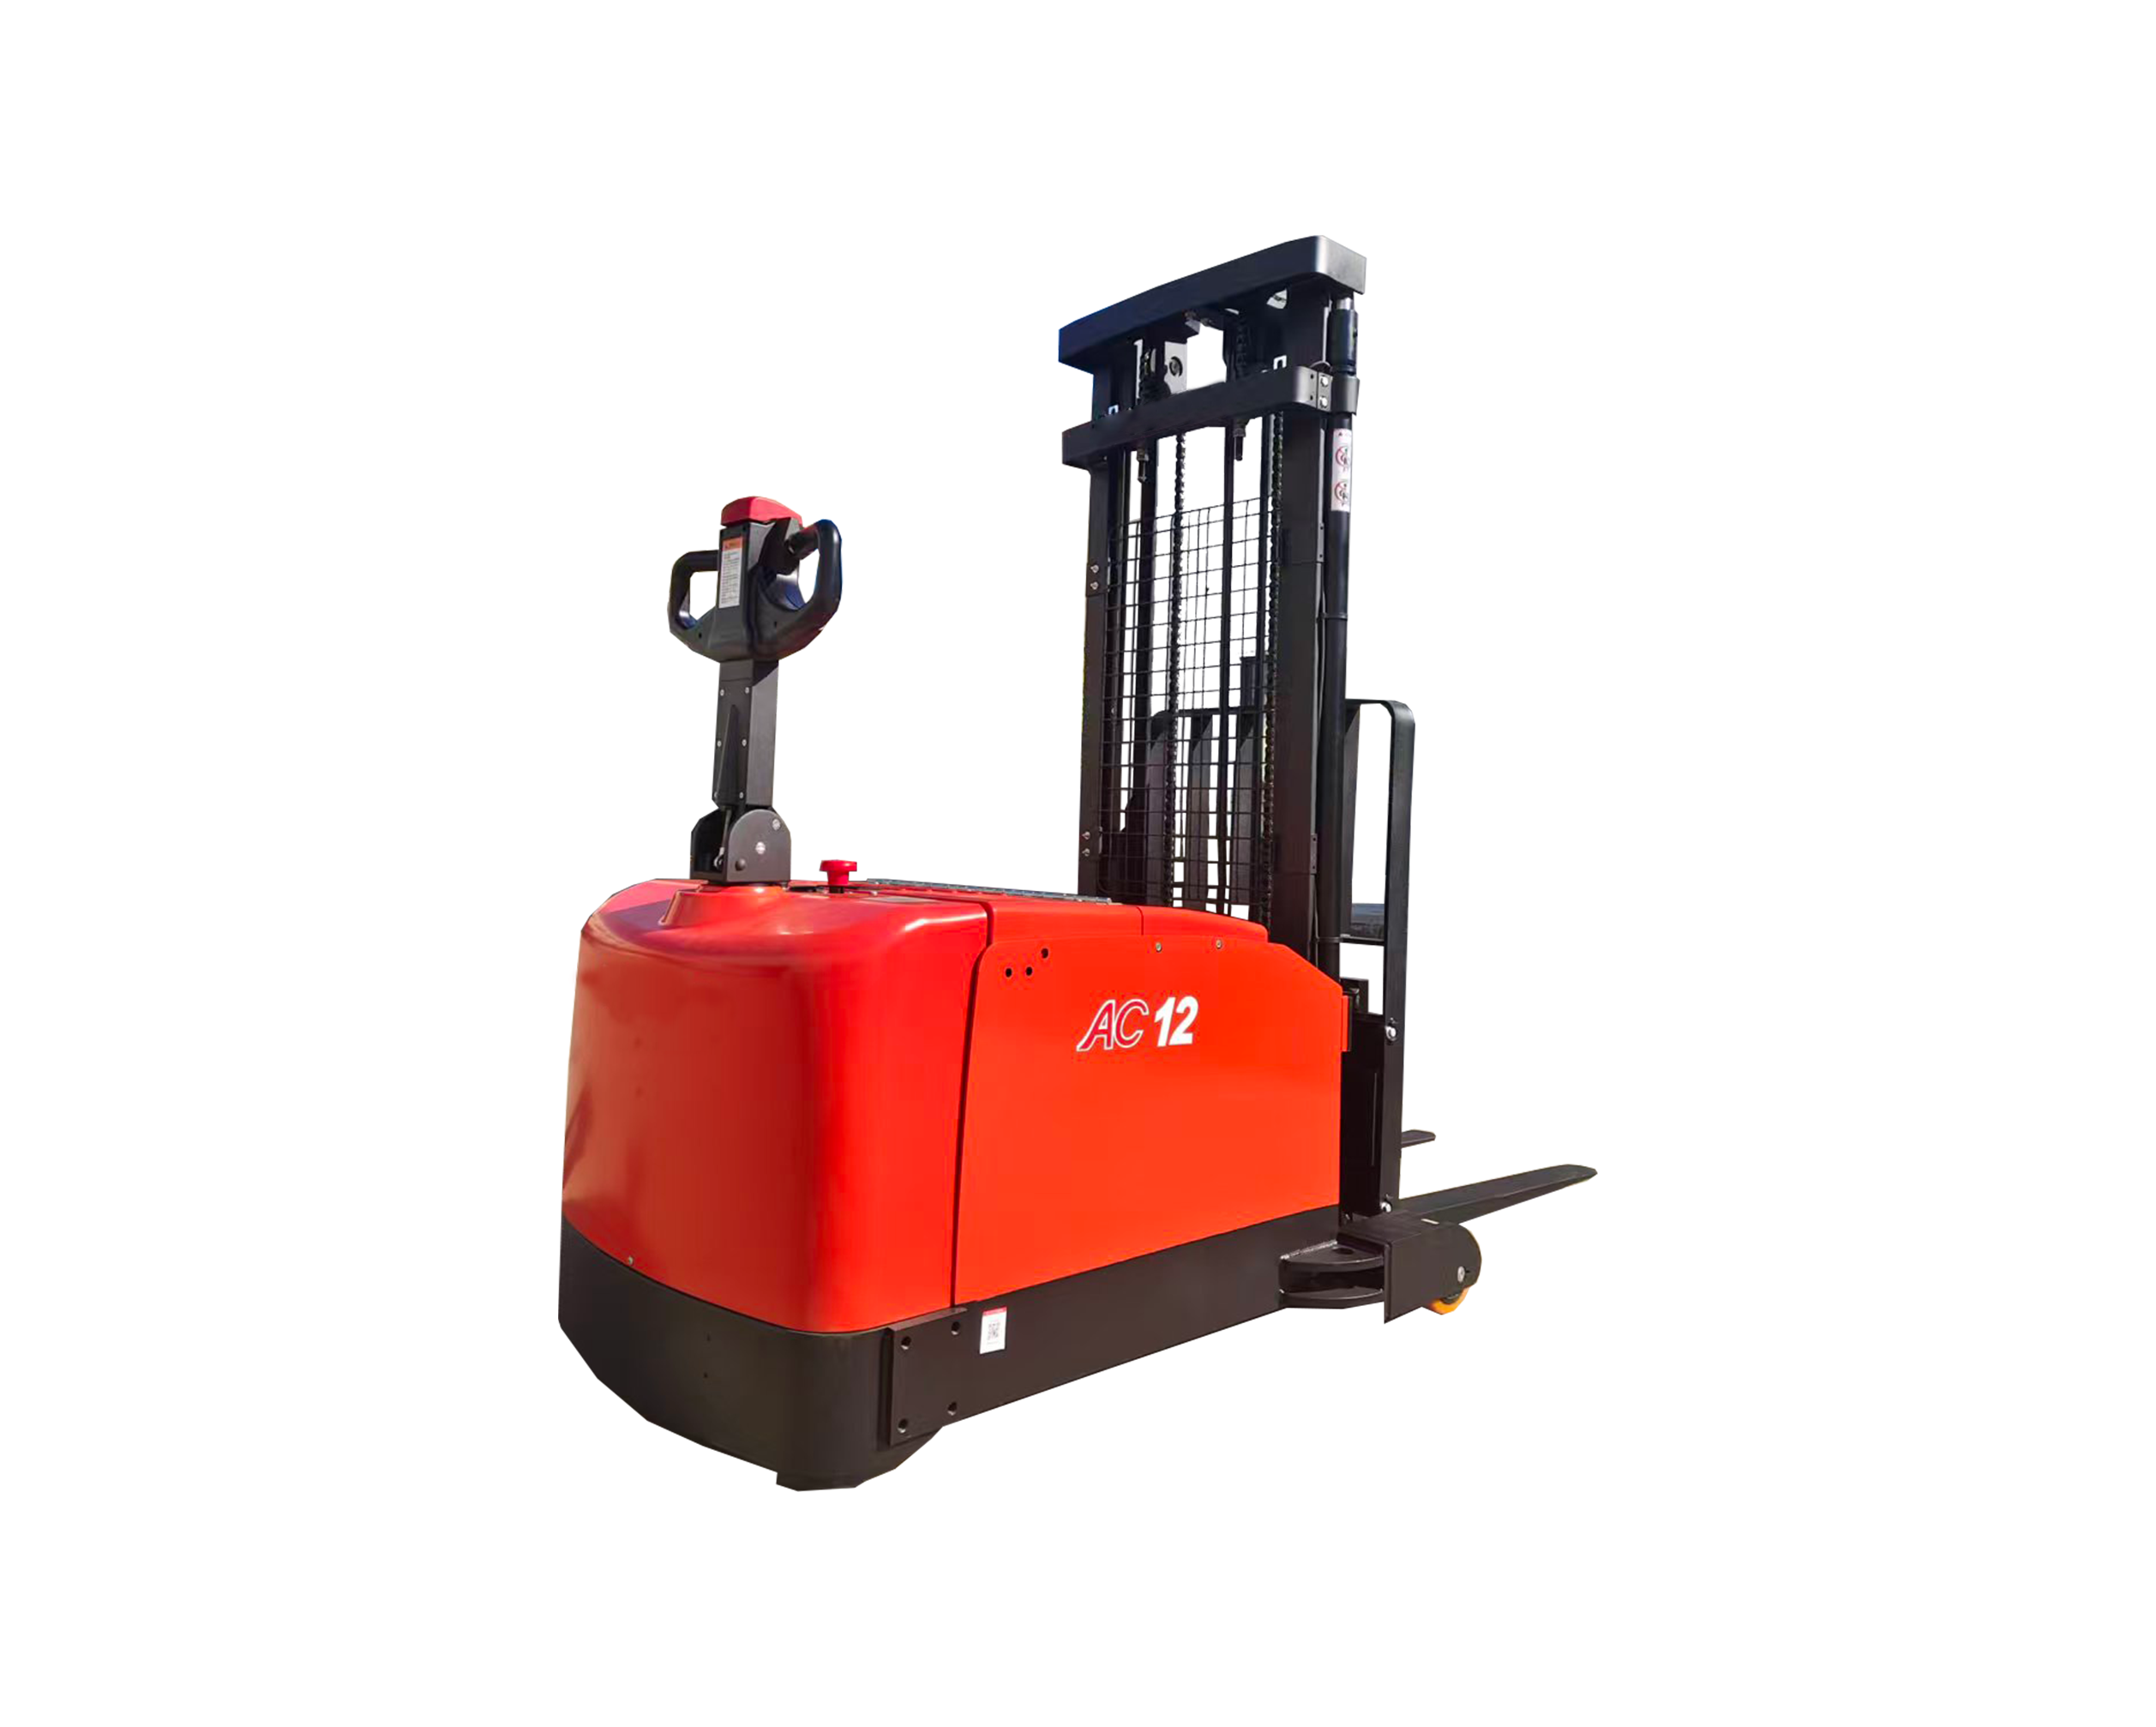
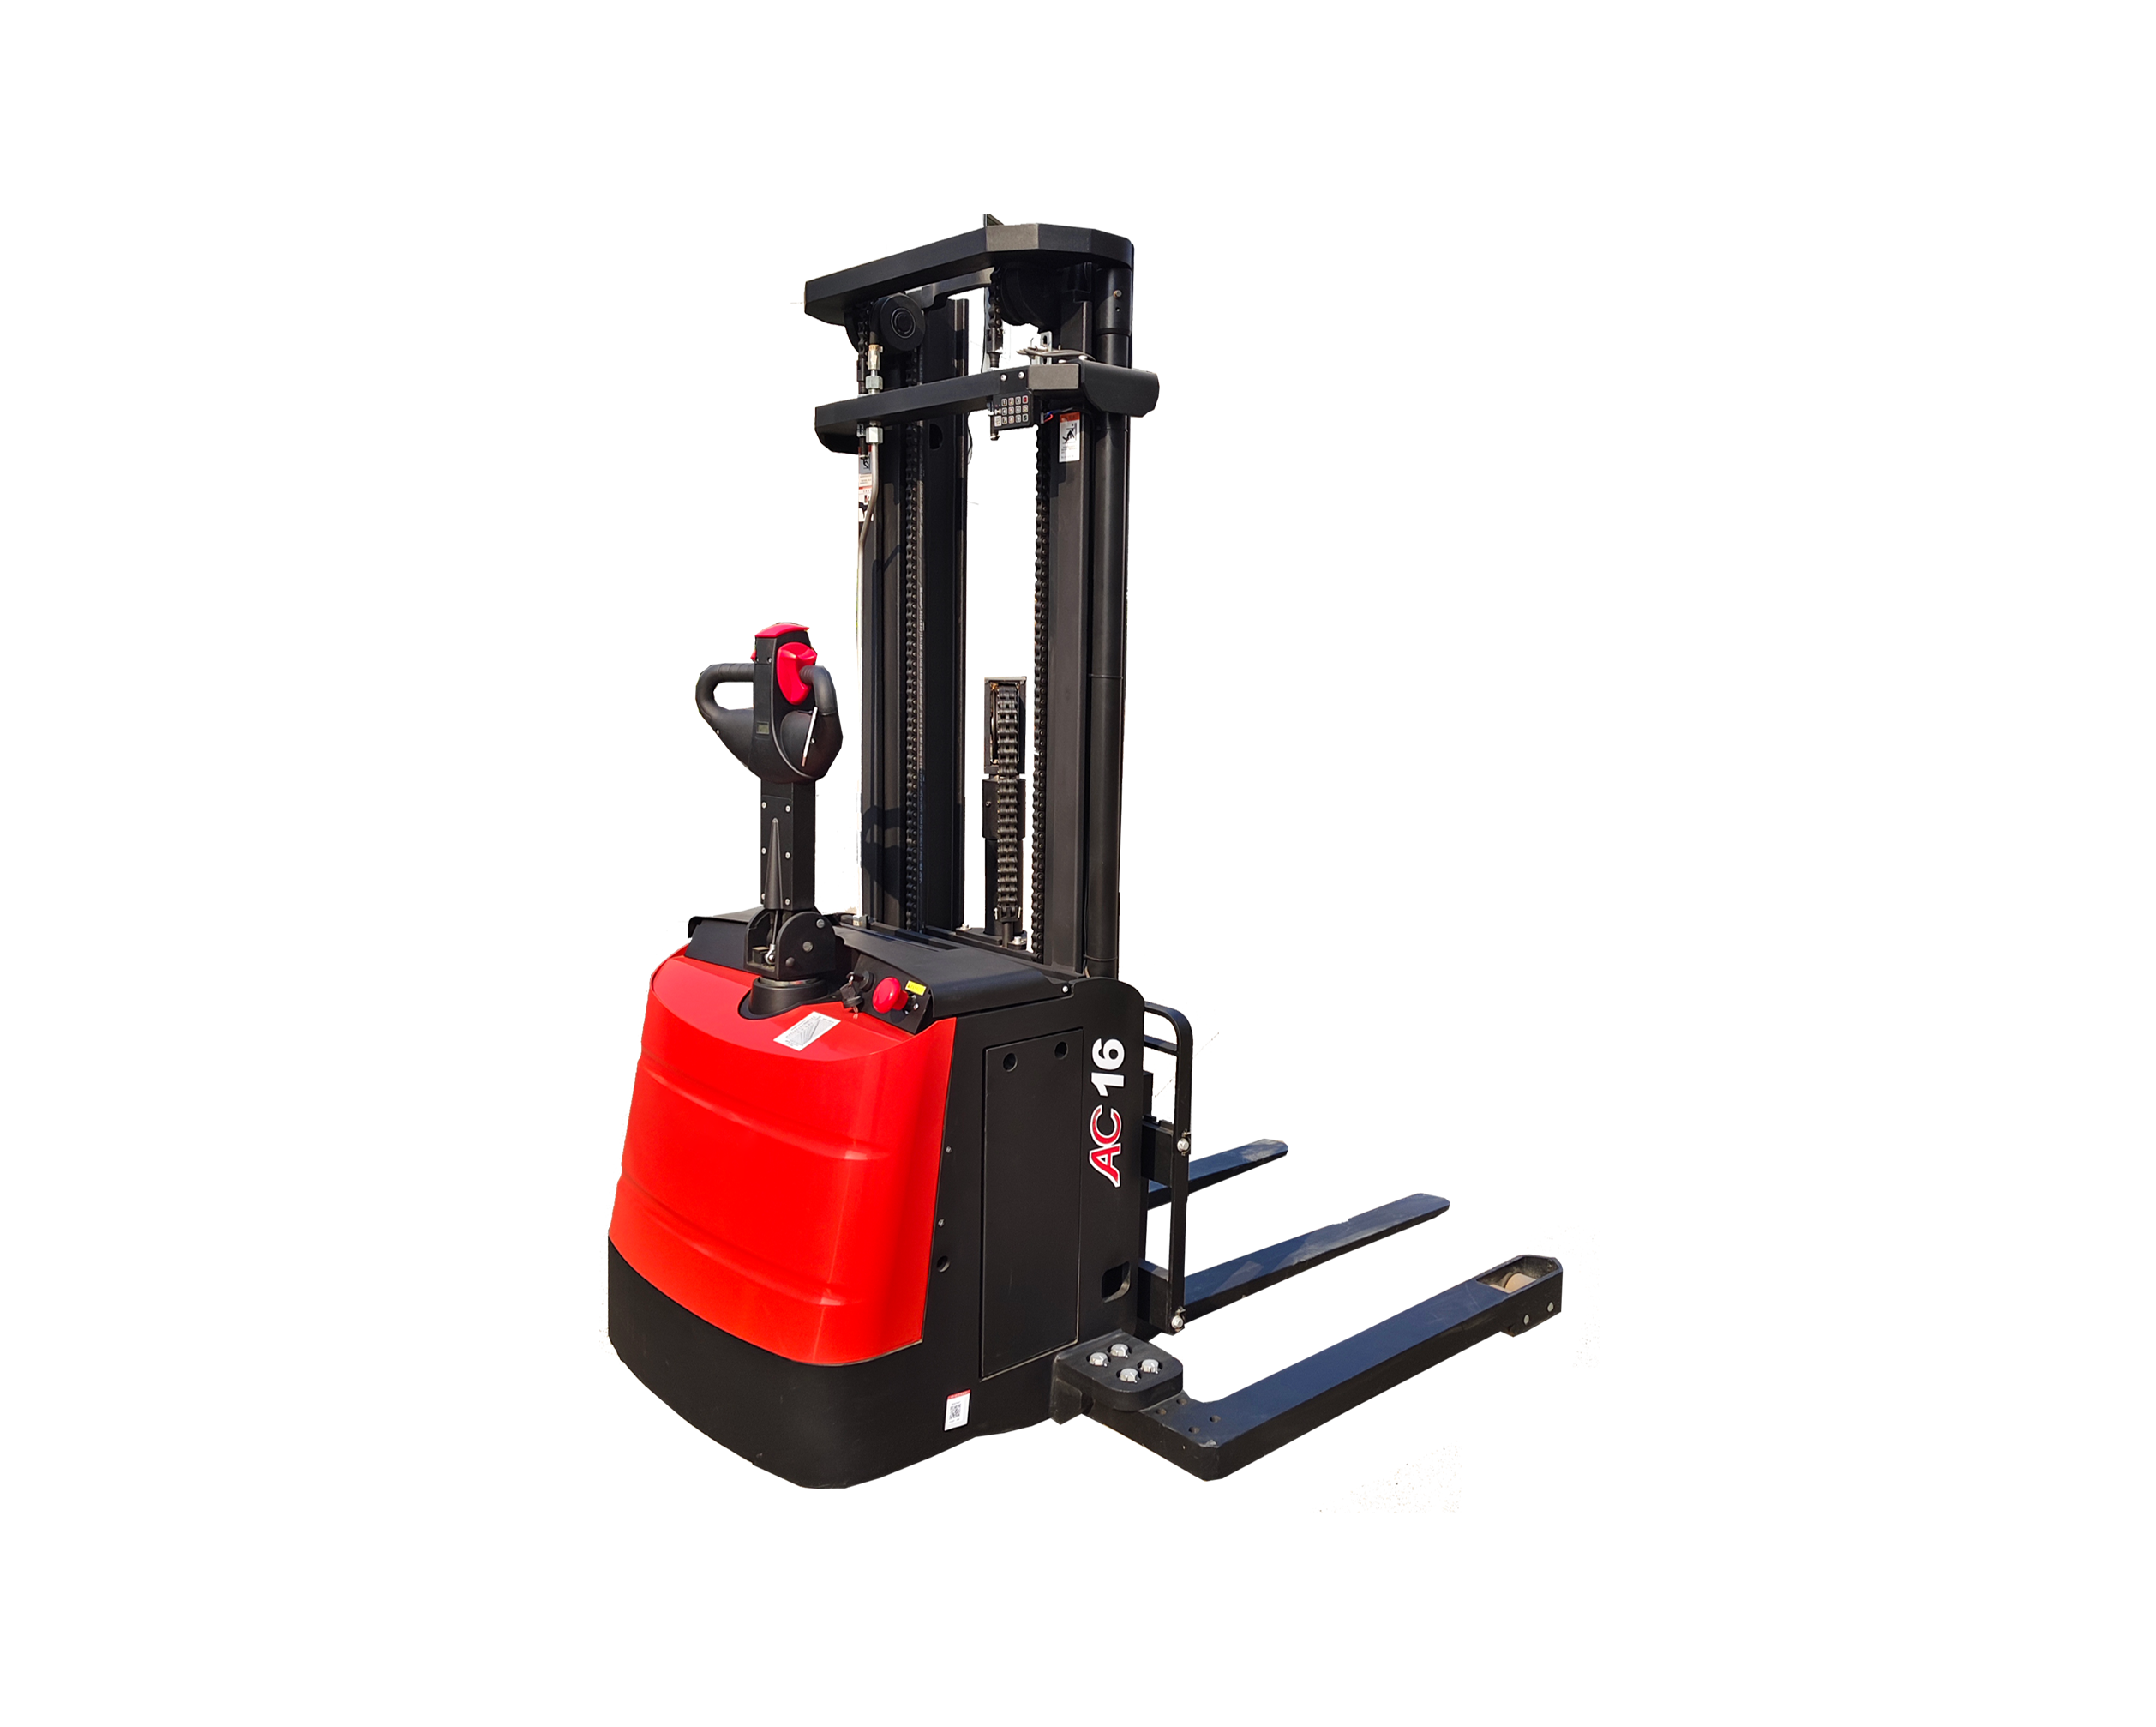
Make better use of vertical storage space while maintaining efficient material flow. Our Electric Stackers support pallet storage and retrieval in warehouses where space utilization and organized inventory management are important.
Food & Beverage Distribution
Handle packaged food, beverages, ingredients, and other goods efficiently throughout distribution centers. Electric pallet trucks and stackers help streamline pallet movement between receiving, storage, picking, and dispatch areas.
Pharmaceutical Logistics
Support the careful movement of pharmaceutical products, medical supplies, and packaged healthcare goods. Electric material handling equipment provides controlled and efficient pallet movement within warehouses and distribution facilities.
Order Picking & Dispatch
Keep temperature-sensitive orders moving efficiently from storage to staging and dispatch. Compact electric equipment helps operators transport pallets and goods between picking areas, cold rooms, staging zones, and loading docks.
3. The Unilift Cold Chain Advantage
Why businesses in temperature-sensitive logistics choose Unilift for material handling operations:
| Feature | Cold Chain Benefit |
|---|---|
| Electric Drive System | Zero exhaust emissions help maintain a cleaner working environment in enclosed warehouses and logistics facilities. |
| Lithium-Ion Ready | Lithium battery options support frequent handling operations and flexible opportunity charging during scheduled breaks. |
| Compact Design | Helps operators maneuver efficiently through narrow aisles, cold rooms, storage areas, and loading zones. |
| Low-Noise Operation | Reduced operating noise helps create a more comfortable working environment in warehouses and distribution facilities. |
| Durable Construction | Robust components are designed to support demanding daily pallet handling and material movement. |
| Flexible Configuration | Fork dimensions, load capacities, and equipment configurations can be adapted to different pallet sizes and application requirements. |
4. Safety & Operational Reliability
Stable Load Handling: Designed to provide controlled and stable pallet movement during loading, storage, picking, and transportation operations.
Operator-Focused Controls: Intuitive controls help operators perform repetitive material handling tasks efficiently and with greater control.
Application-Based Configuration: Equipment specifications can be selected according to load capacity, fork dimensions, aisle conditions, operating environment, and handling frequency.
Cold Chain Application Support: Equipment selection can be adapted to the operational requirements of temperature-controlled warehouses and distribution environments.
Custom MHE Solutions: Unilift MHE can provide customized equipment configurations for different food, pharmaceutical, warehouse, and logistics applications.
From cold storage and food distribution to pharmaceutical warehousing and temperature-controlled logistics, Unilift MHE electric material handling solutions help businesses move temperature-sensitive goods efficiently while supporting clean, organized, and reliable warehouse operations.